How to Choose the Right Conveyor Belt for Industrial Applications
Selecting the right belt is essential for maintaining smooth material handling, improving productivity, and reducing downtime in industrial operations. Different industries require reliable solutions to transport materials safely and efficiently.
A Conveyor Belt plays a vital role in manufacturing, warehousing, mining, and material processing. Choosing a suitable belt depends on the type of material, operating environment, load capacity, and required speed. A high-quality Rubber Conveyor Belt is often preferred for its flexibility, durability, and resistance to demanding working conditions.
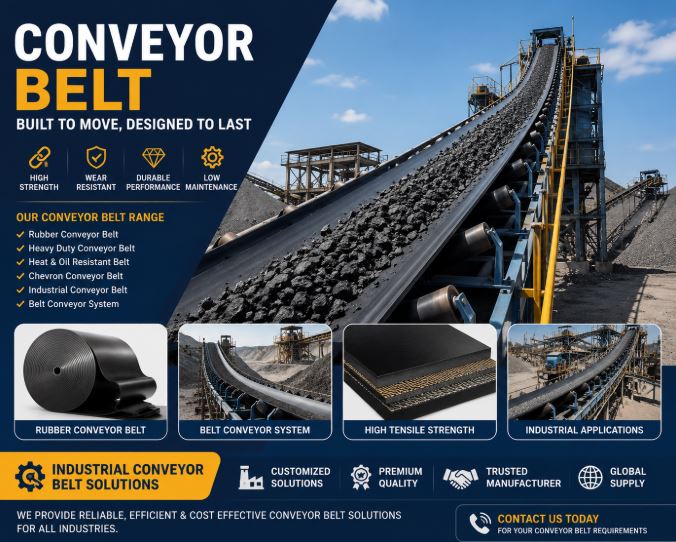
When selecting an Industrial Conveyor Belt, businesses should consider abrasion resistance, belt strength, temperature exposure, and maintenance requirements. Heavy materials and continuous operations may require a Heavy Duty Conveyor Belt designed to withstand demanding workloads. Working with an experienced Conveyor Belt Manufacturer can help businesses identify suitable materials and specifications for their applications.
A dependable Conveyor Belt Supplier can also provide guidance on belt selection, installation requirements, and replacement options. Proper maintenance, regular inspections, and correct belt tension help extend service life and support consistent performance.
Modern Conveyor Belt Systems improve workflow by reducing manual handling and supporting efficient material movement. Whether upgrading an existing Belt Conveyor System or planning a new installation, choosing the right belt can contribute to operational efficiency, safety, and long-term value.
Discover how to choose durable conveyor belts for industrial applications by considering material handling needs, load capacity, operating conditions, and maintenance.